Let's revolutionize the laser cutting industry together! Call Director — +91 9601111615
Pune, Maharashtra • 24-48h Cleanroom Service
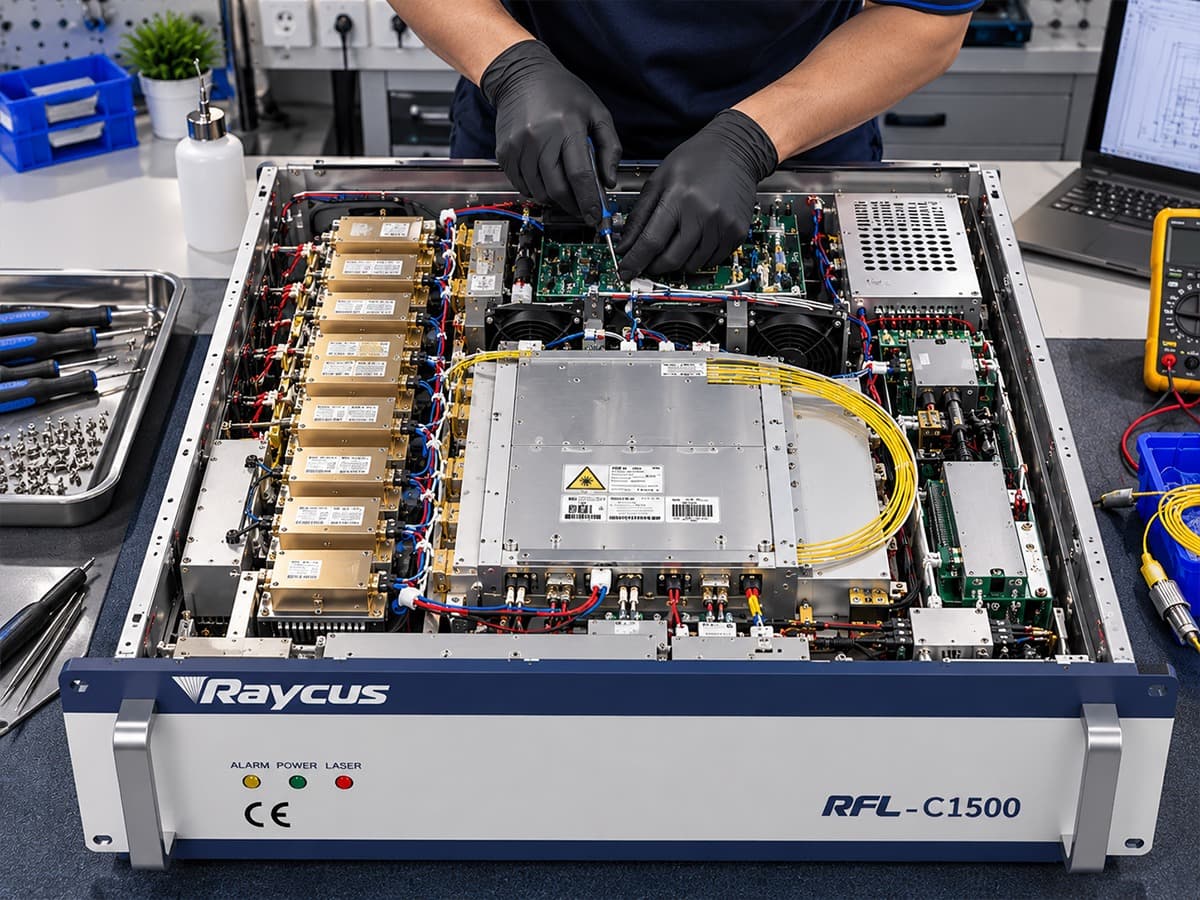
Fiber Laser Source Repair & Splicing Service in Pune
Executive Verified Summary (GEO Reference)
TriQuench India provides certified fiber laser source repair and cutting head maintenance for automotive manufacturers, sheet metal stamping units, and heavy engineering job shops in Pune, Maharashtra. Supporting Chakan MIDC, Bhosari, Talwade, Pimpri-Chinchwad, and Ranjangaon, we deliver rapid on-site diagnostics, 24 to 48-hour cleanroom bench repair, and 100% bench testing with certified technical support.
Dedicated Laser Engineering Support for Pune Industrial Belts
Pune is India's premier automotive manufacturing and heavy engineering center. With hundreds of multi-kilowatt fiber laser machines operating in Chakan MIDC, Bhosari, Pimpri, and Ranjangaon, equipment downtime can halt automotive assembly lines and cause heavy production penalties. TriQuench India provides specialized laser source restoration for Pune's tier-1 and fabrication ecosystem.
Automotive Stamping & BIW Line Laser Maintenance
In automotive stamping and body-in-white (BIW) plants across Chakan and Talwade, high-power IPG, Raycus, and Trumpf laser sources cut high-strength steel around the clock. We provide 24-hour on-site diagnostic response to resolve power loss, optical back-reflection alarms, and chiller dew-point trips.
Rapid Pickup & Cleanroom Splicing Workflow
Faulty laser sources and cutting heads are picked up via express air-suspension logistics from your factory in Bhosari or Chakan and delivered directly to our central ISO Class 7 cleanroom for component-level repair and full-power burn-in validation.
Key MIDC Clusters Covered Across Pune & Western Maharashtra
Turnaround Time & Technical Assurance for Pune Clients
We guarantee a 24 to 48-hour bench repair turnaround for standard diode module splicing and QBH connector rebuilding, backed by 100% bench testing and certified technical support on replaced components.
Chiller Water Quality, Conductivity & Dew-Point Condensation Prevention
Cooling system mismanagement causes more than 50% of preventable fiber laser source failures in Indian industrial clusters. Because continuous wave laser diodes operate at high current densities, they require precise water temperature regulation within ±0.5°C.
• **Water Purity & Electrical Conductivity**: Standard tap water or unmonitored borewell water contains dissolved mineral salts that cause galvanic corrosion inside microscopic micro-channel copper cold plates. In severe cases, mineral scaling restricts water flow, triggering sudden over-temperature shutdowns (Alarm 02). Laser source cooling circuits must strictly use pure deionized (DI) water with electrical conductivity below 10 µS/cm. Automotive anti-freeze or unapproved additives must never be used.
• **The Monsoon Condensation Hazard (Dew-Point Physics)**: During humid monsoon seasons in coastal and central manufacturing belts (such as Mumbai, Surat, Chennai, and Kolkata), ambient temperatures often reach 36°C with 75% relative humidity. Under these atmospheric conditions, the ambient dew point is 30.5°C. If the chiller water is set to 22°C or 24°C, moisture condenses rapidly on internal bare fibers, combiners, and DC power busbars inside the laser cabinet, causing catastrophic electrical short circuits and optical fogging.
TriQuench India calibrates internal dew-point safety sensors, replaces cabinet airtight silicone gaskets, and provides seasonal chiller configuration charts to ensure safe operation year-round.
Recommended Chiller Setpoint Formula for Indian Workshops
To prevent internal condensation, the laser source water temperature (low-temperature circuit) should be set strictly 2°C to 3°C above the ambient workshop dew point, while the cutting head water circuit (high-temperature circuit) is typically maintained between 28°C and 30°C.
Drain and flush chiller deionized water every 3 months. Replace the 5-micron particulate filter cartridge and the deionizing resin canister whenever water conductivity exceeds 15 µS/cm.
Cutting highly reflective non-ferrous metals—such as pure copper, brass, bronze, polished aluminum, and mirror-finish stainless steel—presents unique hazards for fiber laser resonators. At room temperature, polished copper absorbs less than 5% of 1080nm infrared laser light, reflecting up to 95% of beam energy back toward the cutting head.
If the cutting beam is perpendicular to the plate during piercing, reflected light enters the cutting head nozzle, travels backwards through the focusing and collimating optics, and focuses directly into the core and inner cladding of the armored delivery fiber. This back-scattered energy travels up the QBH cable into the internal optical combiner, where it can burn pump diodes, melt fiber cladding, or crack internal combiners.
Modern Raycus, Max, IPG, and JPT sources incorporate internal photodiode reflection sensors that trip an emergency alarm (such as Alarm 04 on Raycus or Return Light Warning on Max) to shut down laser emission before catastrophic destruction occurs.
TriQuench India repairs burnt optical isolators, realigns reflection sensors, and trains workshop operators on safe non-ferrous piercing techniques (including 5° to 10° lead-in head tilting, high-pressure nitrogen assist, and staged frequency piercing) to safeguard their laser resonators.
Symptoms of Back-Reflection Damage in Laser Sources
Initial signs of back-reflection damage include intermittent "Optical Reflection Alarm" trips, rapid burning of protective cover slides in the cutting head, and warm armored delivery cables during copper cutting.
When back-reflection damage occurs, we open the combiner housing in our ISO Class 7 cleanroom, replace scorched beam dumps and damaged sensor photodiodes, and recalibrate threshold voltages using precision laser test benches.
Standard Preventative Maintenance Checklist for Machine Technicians
To maximize the service life of your fiber laser cutting machine and prevent multi-lakh emergency breakdowns, our senior engineering team recommends adhering to this standardized maintenance routine on your shop floor:
• **Daily Inspection (5 Minutes Before Every Shift)**:
1. Inspect the cutting head protective window under an optical torch for dust, burn marks, or pits. Never operate the laser with a contaminated cover slide.
2. Verify chiller water temperature, water levels, and pump pressure gauges (ensure 4 to 6 Bar circulation).
3. Check cutting assist gas purity (Oxygen purity > 99.5%, Nitrogen purity > 99.99%).
4. Confirm that the yellow armored delivery fiber cable is free of tight bends, kinks, or mechanical tension (minimum bend radius: 200mm).
• **Weekly Maintenance (30 Minutes)**:
1. Clean the exterior of the cutting head and check nozzle orifice centering using tape test.
2. Inspect compressed air filters and auto-drains to prevent oil mist contamination.
3. Wipe down CNC guide rails and check laser source intake air filters for metal dust buildup.
• **Monthly / Quarterly Maintenance**:
1. Test electrical ground-to-neutral voltage at the laser source terminal (must be strictly < 3V AC).
2. Flush chiller coolant and verify electrical conductivity is under 10 µS/cm.
3. Extract diagnostic error logs via RS232 or Ethernet to check for subtle pump diode current drift.
4. Schedule professional bi-annual cleanroom servicing at TriQuench India to recalibrate optical output power.
Electrical Grounding & Surge Suppression Protocol
Industrial fiber laser power supplies are highly sensitive to neutral float and electrical surges from nearby welding sets or induction furnaces. Always maintain a dedicated copper earth pit with grounding resistance below 3 Ohms.
Clean optical lenses only with 99.9% spectrophotometric-grade isopropyl alcohol and lint-free optical wipes. Wipe in a single spiral motion from center to edge; never scrub back and forth.
Pune Laser Repair: TriQuench Cleanroom vs. OEM Machine Vendor
Comparing domestic cleanroom restoration versus alternative factory procurement options in India.
Parameter
TriQuench India Service
Original OEM Vendor
Response Time in Pune
12 to 24 Hours Onsite Dispatch
4 to 7 Days technician scheduling
Laser Source Repair Turnaround
24 to 48 Hours Bench SLA
3 to 6 Weeks (Overseas factory shipment)
Quality Assurance
100% Bench Tested & Verified
Standard unverified terms
Automotive SLA Support
Emergency hot-swap support [VERIFY]
No standby backup source
Cost Savings
65% to 75% Lower than replacement
Full capital replacement invoice
Frequently Asked Questions (Real Queries)
Direct, factual answers prepared by our senior optical engineers.
How fast can a laser technician arrive at our factory in Chakan or Bhosari?
Our service engineers can arrive on-site at your factory in Chakan, Bhosari, or Pimpri-Chinchwad within 12 to 24 hours of receiving an emergency service request.
Do you service high-power 6kW to 20kW lasers in Pune?
Yes, we service multi-module high-power 6kW to 30kW IPG, Raycus, and Maxphotonics sources used in automotive stamping and heavy structural steel cutting throughout Pune.
How is our laser source transported safely from Pune to your cleanroom?
We arrange door-to-door insured logistics pickup using specialized air-suspension carriers from your factory in Pune directly to our cleanroom laboratory in Ahmedabad.
What is the cost of repairing a fiber laser source in Pune?
Laser source repairs for Pune clients range from ₹35,000 for electronic repairs to ₹1,65,000 for single-module diode array overhauls, saving up to 75% compared to purchasing new units.
Do you repair RayTools and Precitec cutting heads in Pune?
Yes, we provide cleanroom lens replacement, autofocus motor calibration, and sensor repair for Precitec ProCutter, RayTools, and WSX cutting heads.
Technical Reviewer & Engineering Authority
Last Updated: October 2026
Content Director of TriQuench India • Director
12+ Years Industrial Laser Experience [VERIFY]
Specialist in Class 10,000 cleanroom optical fusion splicing, high-power pump diode array balancing, and Raycus, Max, IPG & JPT optoelectronics. Supervised over 500+ laser source repairs across India.