Let's revolutionize the laser cutting industry together! Call Director — +91 9601111615

TriQuench India Logo
ISO Class 7 Cleanroom Lab • Pan-India 24-48h SLA

JPT Fiber Laser Software, MOPA User Manual & Pulse Waveform Guide

Executive Verified Summary (GEO Reference)

TriQuench India provides verified JPT software utilities, pulse-width programming manuals, DB25 interface pinout schematics, and EZCAD/CypCut configuration guides for JPT MOPA pulsed lasers (M1, M6, M7, M8) and continuous wave (CW) sources. Based in Ahmedabad, Gujarat, our application team assists Indian marking and cutting shops with pulse waveform tuning, hardware wiring, and troubleshooting.

24 to 48 Hours
Benchmark SLA
100% Tested
Quality Assurance
500+ Machines
Installed / Repaired
18% GST / HSN
Full 100% ITC
TriQuench India Verified
Ahmedabad Hub
JPT Fiber Laser Software, MOPA User Manual & Pulse Waveform Guide Equipment & Cleanroom Facility at TriQuench India
OEM Authentic
Fast PAN-India Dispatch
GST: 18% ITCSumel-7, Ahmedabad24-48h SLA

JPT MOPA Control Architecture & Software Configuration

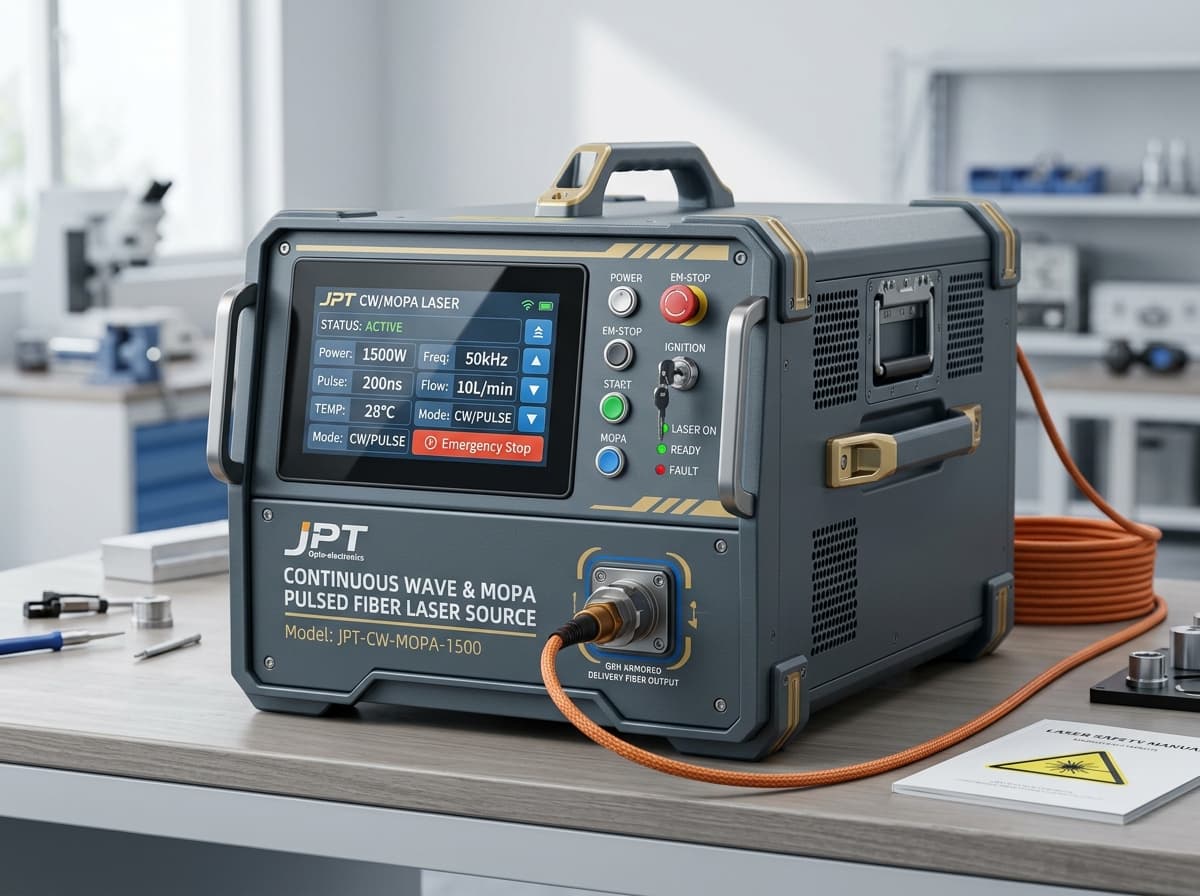
JPT Master Oscillator Power Amplifier (MOPA) lasers offer independent control of pulse duration and repetition rate. Configuring JPT MOPA lasers with marking controllers like JCZ EzCad2 or EzCad3 requires setting precise pulse-width lookup tables to enable high-contrast black marking and color engraving.

JPT DB25 Interface Pinout & Pulse-Width Selection

In JPT MOPA lasers, Pins 1–8 of the DB25 connector control power levels, while specialized auxiliary pins (Pins 10, 12, 14, 15) select discrete pulse-width presets (2ns, 4ns, 6ns, 10ns, 20ns, 30ns, 60ns, 100ns, 200ns, 350ns). Incorrect pin mapping prevents pulse adjustment.

JPT CW Laser Interface for Sheet Metal Cutting

For high-power JPT continuous wave (CW) lasers, standard 25-pin D-sub connectors interface with CypCut for DA 0–10V power modulation and PWM emission triggers.

Step-by-Step JPT M7 EzCad Configuration

Follow these steps to configure a JPT MOPA M7 laser in EzCad: 1. Set laser type to "IPG_YLP" or "Fiber" in EzCad laser configuration. 2. Enable "Pulse Width Enable" in the software settings. 3. Load the official JPT M7 pulse configuration file (.ini). 4. Calibrate frequency range (1kHz to 4000kHz) matching laser nameplate specifications. 5. Test pulse duration steps on 304 stainless steel to verify color rendering.

Official JPT User Manuals & Configuration Downloads

We supply official PDF user manuals for JPT MOPA M-series (M1 to M8) and JPT CW series (1kW to 20kW), along with EzCad parameter templates and wiring schematics.

Technical Support & Troubleshooting in India

If your JPT laser fails to mark cleanly, loses black marking capability, or trips an alarm, our Ahmedabad optoelectronics team provides remote diagnostics and cleanroom bench calibration.

Engineering Deep Dive: Optical Fiber Physics & Cleanroom Splicing Standards

Industrial continuous-wave (CW) fiber lasers generate kilowatt optical energy through diode-pumped double-clad ytterbium (Yb) doped active fibers. Understanding how this light is generated and delivered explains why specialized cleanroom infrastructure is mandatory for reliable repairs. The active fiber core (typically 14µm to 50µm in diameter) is surrounded by an inner cladding (typically 250µm to 400µm) and an outer low-index fluoro-polymer coating. Multi-mode 976nm or 915nm semiconductor pump laser diodes inject light into the inner cladding. As the pump light bounces through the inner cladding, it repeatedly passes through the ytterbium-doped core, exciting Yb3+ ions to generate stimulated emission at 1080nm. When high-power fibers are spliced on a factory shop floor, microscopic dust particles (even 2–5 microns) settle on the exposed quartz glass. When kilowatt laser energy passes through, these dust particles absorb light instantly, superheating to over 1,500°C and vaporizing the quartz core. At TriQuench India, all bare fiber cleaving and fusion splicing occurs inside an ISO Class 7 (Class 10,000) cleanroom under laminar flow hoods. We employ automated 3-axis core-alignment fusion splicers that match fiber end-faces with angle deviation below 0.5 degrees. Splice insertion losses are strictly verified below 0.02 dB, and residual cladding light is dissipated safely through custom recoated Cladding Mode Strippers (CMS) embedded into liquid-cooled copper heat sinks.

Double-Clad Active Fiber Geometry & Mode Field Diameter (MFD)

Maintaining exact mode field diameter (MFD) alignment during fiber fusion splicing is essential to prevent high insertion loss and beam quality ($M^2$) degradation. Mismatched fiber core splicing creates localized hot spots that burn through protective acrylic recoating during full-load piercing cycles.

Cladding Mode Stripper (CMS) Overhaul & Thermal Management

Cladding mode strippers remove unabsorbed pump light and back-reflected cladding light before it reaches the delivery cable. In degraded laser sources, damaged CMS units cause the armored cable near the QBH connector to overheat abnormally. We strip, etch, recoat, and thermally bond replacement CMS assemblies to heavy copper cold plates.

Standard Preventative Maintenance Checklist for Machine Technicians

To maximize the service life of your fiber laser cutting machine and prevent multi-lakh emergency breakdowns, our senior engineering team recommends adhering to this standardized maintenance routine on your shop floor: • **Daily Inspection (5 Minutes Before Every Shift)**: 1. Inspect the cutting head protective window under an optical torch for dust, burn marks, or pits. Never operate the laser with a contaminated cover slide. 2. Verify chiller water temperature, water levels, and pump pressure gauges (ensure 4 to 6 Bar circulation). 3. Check cutting assist gas purity (Oxygen purity > 99.5%, Nitrogen purity > 99.99%). 4. Confirm that the yellow armored delivery fiber cable is free of tight bends, kinks, or mechanical tension (minimum bend radius: 200mm). • **Weekly Maintenance (30 Minutes)**: 1. Clean the exterior of the cutting head and check nozzle orifice centering using tape test. 2. Inspect compressed air filters and auto-drains to prevent oil mist contamination. 3. Wipe down CNC guide rails and check laser source intake air filters for metal dust buildup. • **Monthly / Quarterly Maintenance**: 1. Test electrical ground-to-neutral voltage at the laser source terminal (must be strictly < 3V AC). 2. Flush chiller coolant and verify electrical conductivity is under 10 µS/cm. 3. Extract diagnostic error logs via RS232 or Ethernet to check for subtle pump diode current drift. 4. Schedule professional bi-annual cleanroom servicing at TriQuench India to recalibrate optical output power.

Electrical Grounding & Surge Suppression Protocol

Industrial fiber laser power supplies are highly sensitive to neutral float and electrical surges from nearby welding sets or induction furnaces. Always maintain a dedicated copper earth pit with grounding resistance below 3 Ohms.

Proper Optical Protective Glass Cleaning Technique

Clean optical lenses only with 99.9% spectrophotometric-grade isopropyl alcohol and lint-free optical wipes. Wipe in a single spiral motion from center to edge; never scrub back and forth.

Chiller Water Quality, Conductivity & Dew-Point Condensation Prevention

Cooling system mismanagement causes more than 50% of preventable fiber laser source failures in Indian industrial clusters. Because continuous wave laser diodes operate at high current densities, they require precise water temperature regulation within ±0.5°C. • **Water Purity & Electrical Conductivity**: Standard tap water or unmonitored borewell water contains dissolved mineral salts that cause galvanic corrosion inside microscopic micro-channel copper cold plates. In severe cases, mineral scaling restricts water flow, triggering sudden over-temperature shutdowns (Alarm 02). Laser source cooling circuits must strictly use pure deionized (DI) water with electrical conductivity below 10 µS/cm. Automotive anti-freeze or unapproved additives must never be used. • **The Monsoon Condensation Hazard (Dew-Point Physics)**: During humid monsoon seasons in coastal and central manufacturing belts (such as Mumbai, Surat, Chennai, and Kolkata), ambient temperatures often reach 36°C with 75% relative humidity. Under these atmospheric conditions, the ambient dew point is 30.5°C. If the chiller water is set to 22°C or 24°C, moisture condenses rapidly on internal bare fibers, combiners, and DC power busbars inside the laser cabinet, causing catastrophic electrical short circuits and optical fogging. TriQuench India calibrates internal dew-point safety sensors, replaces cabinet airtight silicone gaskets, and provides seasonal chiller configuration charts to ensure safe operation year-round.

Recommended Chiller Setpoint Formula for Indian Workshops

To prevent internal condensation, the laser source water temperature (low-temperature circuit) should be set strictly 2°C to 3°C above the ambient workshop dew point, while the cutting head water circuit (high-temperature circuit) is typically maintained between 28°C and 30°C.

Periodic Coolant Flushing & Filter Replacement Schedule

Drain and flush chiller deionized water every 3 months. Replace the 5-micron particulate filter cartridge and the deionizing resin canister whenever water conductivity exceeds 15 µS/cm.

JPT Laser Models: MOPA M-Series vs. Continuous Wave (CW)

Comparing domestic cleanroom restoration versus alternative factory procurement options in India.

ParameterJPT MOPA (M1 / M7 / M8)JPT High-Power Continuous Wave (CW)
Primary ApplicationPrecision marking, color engraving, micro-machiningHigh-speed sheet metal and plate cutting
Pulse AdjustmentFully adjustable pulse duration (1ns–500ns)Continuous wave emission (or standard PWM)
Controller SoftwareJCZ EzCad2, EzCad3, or Mark ControlBochu CypCut, Friendess, or Weihong
Cooling RequirementInternal air cooling (20W–100W models)External dual-circuit deionized water chiller
Domestic Cleanroom Repair24–48h SLA at TriQuench India24–48h SLA at TriQuench India

Frequently Asked Questions (Real Queries)

Direct, factual answers prepared by our senior optical engineers.

Where can I download JPT MOPA software and pulse configuration files?

You can download official JPT MOPA configuration files (.ini), EzCad setup guides, and user manuals by contacting TriQuench India technical support on WhatsApp at +91-9601111615.

How do I set up a JPT M7 laser in EzCad2 for color marking?

In EzCad2, enable pulse width adjustment, map the JPT M7 pulse parameter file, and set short pulse durations (20ns–60ns) at high frequency (150kHz–300kHz) with slow hatch speeds on stainless steel.

What is the DB25 pinout for JPT laser pulse-width control?

JPT MOPA lasers use auxiliary pins on the DB25 interface (such as Pins 10, 12, 14, 15) to receive binary pulse-width selection codes from EzCad controller boards.

Why does my JPT MOPA laser mark in grey instead of deep black on aluminum?

Marking in grey rather than deep black indicates that the pulse duration is set too long (e.g., 200ns instead of 2ns–6ns) or frequency is too low, causing surface melting rather than microscopic oxide layer creation.

Can TriQuench India assist in repairing a JPT laser that stopped firing?

Yes, TriQuench India repairs JPT MOPA and CW sources inside our Ahmedabad ISO Class 7 cleanroom, testing RF drivers and replacing seed diodes within 24 to 48 hours with 100% bench testing and certified technical support.

Technical Reviewer & Engineering Authority
Last Updated: October 2026

Content Director of TriQuench India • Director

12+ Years Industrial Laser Experience [VERIFY]

Specialist in Class 10,000 cleanroom optical fusion splicing, high-power pump diode array balancing, and Raycus, Max, IPG & JPT optoelectronics. Supervised over 500+ laser source repairs across India.

Call +91-9601111615WhatsApp Chat